
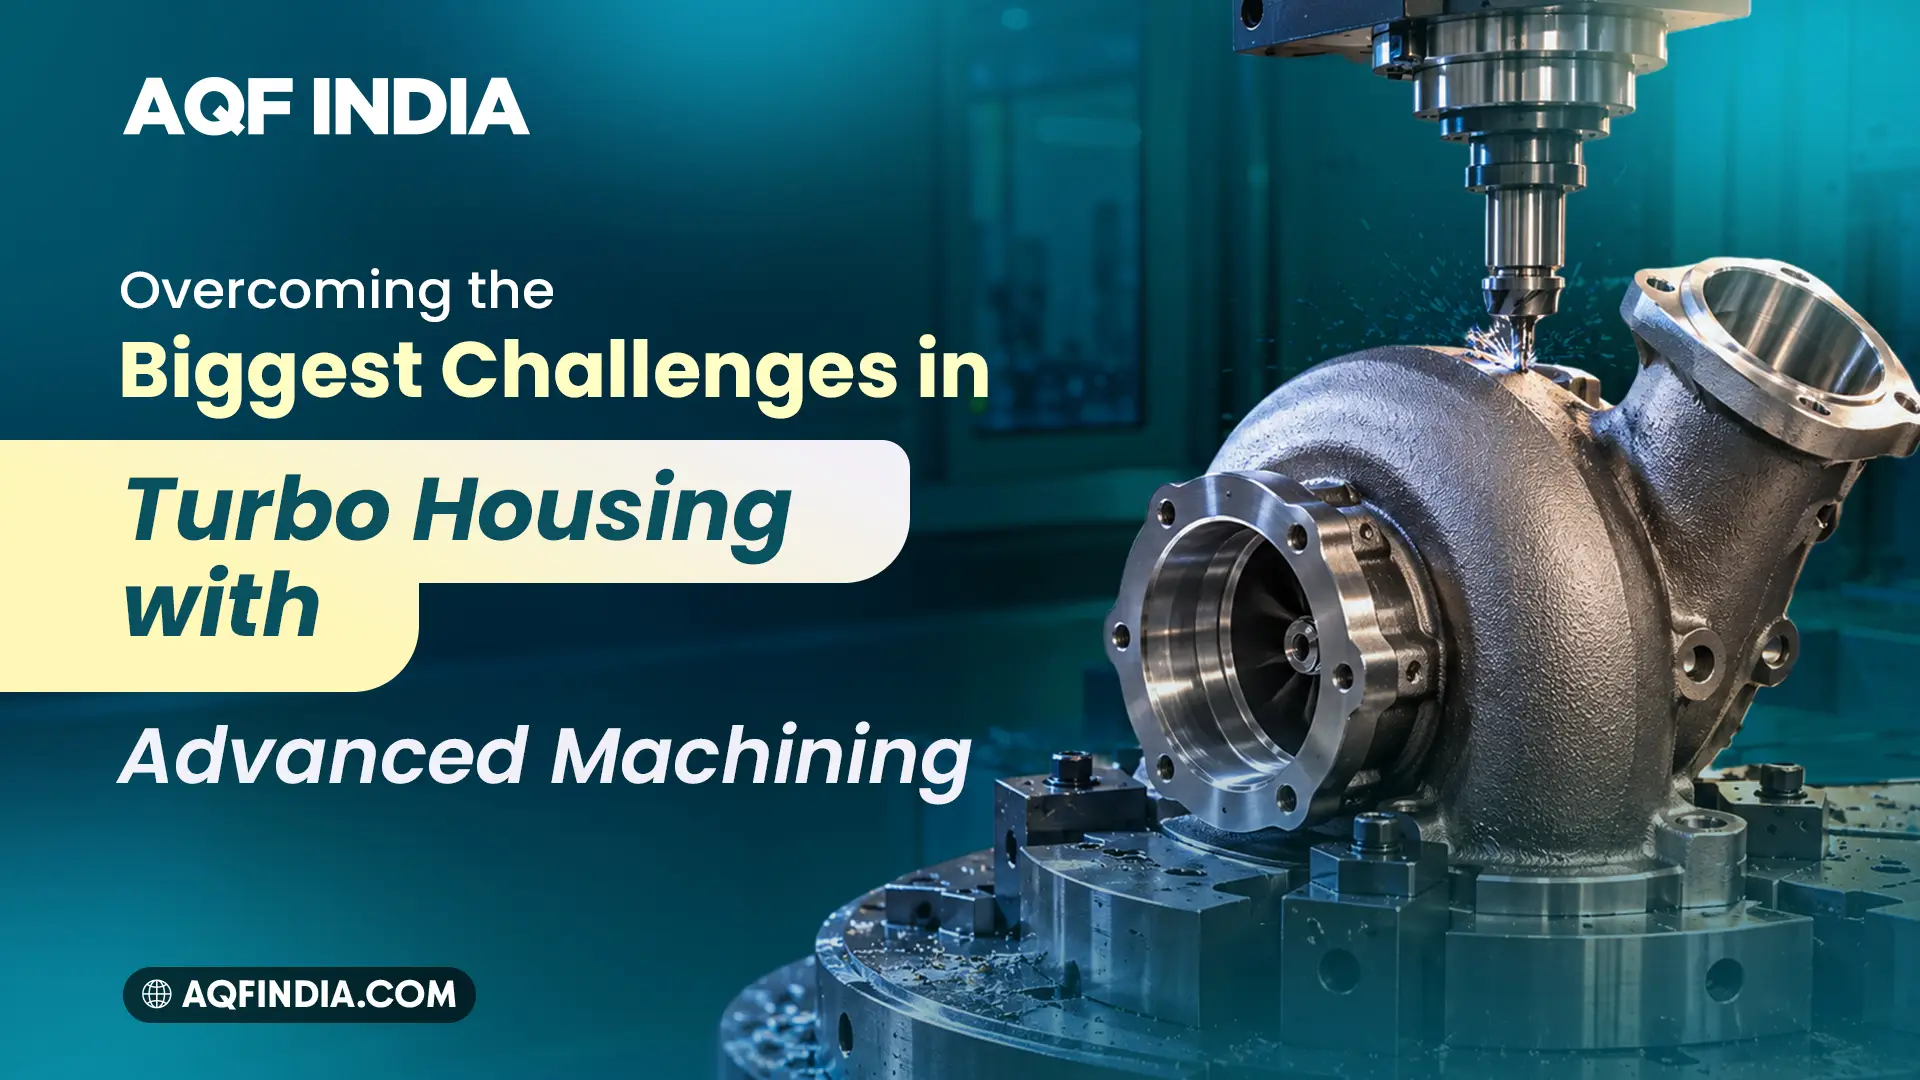
- Turbo housing fabrication tends to go wrong in the same few spots, and most of them show up right at the machine.
- The turbine housing takes the exhaust heat in every turbocharger, which is why the material fights back when you cut it.
- The majority of this scrap is due to worn tools, hard-to-hold shapes, and bore alignment.
- Shaft and housing have to fit each other, so ask your turbine shaft manufacturer how the journals get checked.
- Most of it can be fixed at the machine, if the setup and inspection are planned before cutting starts.
Why the Turbo Housing Is Harder Than It Looks
Open up a turbocharger and the hot half looks almost simple: a cast shell shaped like a snail, a couple of flanges, a few bores. It isn’t simple at all. Anyone who has run a batch of these on a machining centre will tell you the first twenty pieces are fine and the next twenty start drifting.
Most of the trouble comes from four places. We’ll go through them one at a time, with what actually fixes each.
What a Turbine Housing Really Goes Through
The exhaust is emitted from the engine and immediately enters the housing. It has a spiral passage (volute) that accelerates the gas prior to its impact on the turbine wheel that rotates the shaft. Garrett has listed a range of housing materials up to approximately 1,050°C, so it’s cast iron or alloy steel cast for heat resistance. We make high silicon moly (SiMo) manifolds that are rated to 900°C, and the concept is the same.
The catch is simple. Metal that handles heat well tends to chew through cutting tools, and that’s where the trouble begins.
Challenge 1: Materials That Fight Back
These grades are abrasive. Edges wear quickly, and when an edge wears, the bore size creeps with it. Reported tool life on heat-resistant housing steels can be as low as 50 to 125 parts, depending on the operation. Nobody notices a worn edge until the gauge does.
What helps is a mix of small things. Coated carbide grades chosen for the material, light depths of cut, short and stiff tool holders, and plenty of coolant. High-pressure coolant has been reported to stretch finishing tool life several times over. Then comes tool monitoring, so the tool gets changed before the limit and not after the first bad part.
Challenge 2: Awkward Shapes and Interrupted Cuts
The centre housing is an odd piece to hold. Some round features get turned instead of milled, and the V-band groove on the exhaust side means interrupted cutting, where the tool keeps hitting metal and air, metal and air. That shocks the edge every revolution.
Fixtures built around this specific part make the difference. Add hydraulic clamping, minimal tool overhang, and smooth toolpaths, and the vibration drops. A 4th axis helps too, because more faces can be cut in one clamping. Our machine shop handles multi-axis work up to the 4th axis on Doosan and Makino machines for exactly this reason.
Challenge 3: Getting the Bores Right
The centre housing carries the bearing bores, and the sealing faces sit right beside them. The shaft turns at well over a hundred thousand rpm in there. If a bore is slightly out of line, you won’t see it on the bench. You’ll hear it later as noise, or find it as a worn bearing.
So the bores get cut together, in one setup, to keep them concentric. Probes inside the machine check them as we go, and a CMM confirms the final numbers. We fit probes to keep consistency across operations, and the measuring is done in our in-house lab.
Challenge 4: Leaks You Can’t See Until Testing
Castings sometimes hide porosity. Machining opens the surface, and a pinhole that was buried suddenly becomes a leak path. Finding it after assembly is expensive.
Two checks fix most of it. Look at the casting before machining, so obviously bad blanks never reach the machine. Then pressure test the finished part. We run air, water and oil pressure testing as part of our process, which catches leaks while the part is still on our side of the fence.
Don’t Forget the Shaft Inside
The turbine wheel is joined to a shaft, and that shaft runs in the bearings inside the centre housing. Housing bore and shaft journals have to match, and a small mismatch on either side gets paid for by the other.
That’s why it helps to deal with a turbine shaft manufacturer that understands the housing too. We machine shafts by CNC turning and grinding and test them in the lab.
Also Check: The Role of Shafts in Mechanical Systems and Top 7 Common Shaft Problems and How to Fix Them.
What to Ask Before You Pick a Shop
Keep the questions practical. How do you control tool wear on heat-resistant grades? Are critical bores finished in one setup? Do you probe in the machine or only measure at the end? Can you pressure test, and do you check the casting first? Straight answers to those four tell you most of what a brochure won’t.
Final Thought
None of these problems is new, and every one has a known fix. Heat-resistant material, awkward shapes, tight bores, and hidden porosity get handled at the planning stage, before the first cut, or they get handled in scrap later.
Got a turbo housing drawing in hand? Send it across. We’ll tell you how we’d clamp it, cut it and test it, and you can decide from there. Reach AQF India anytime.
FAQs
1. What does a turbine housing do in a turbocharger?
It collects exhaust gas and guides it onto the turbine wheel, which spins the shaft. Because it sits on the hot side, it needs heat-resistant material.
2. How does it make these housings so hard to machine?
They wear quickly, have an awkward shape to clamp, and require tight accuracy for bearing bores and sealing faces.
3. How to identify a good turbine shaft manufacturer?
Turning and grinding work is well controlled; dimensions and surface finish are checked in the laboratory, and shaft journals can be matched to the bores in the housing.